
Product Overview
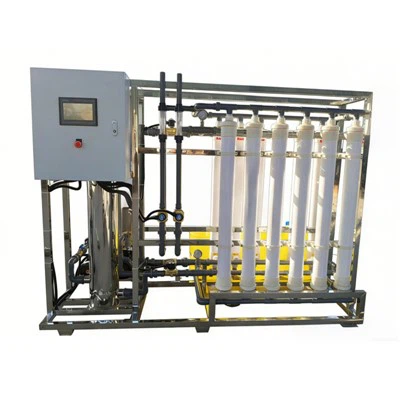
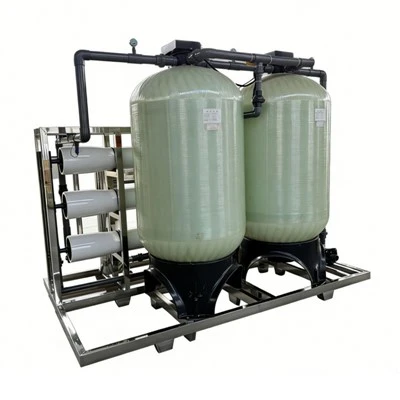
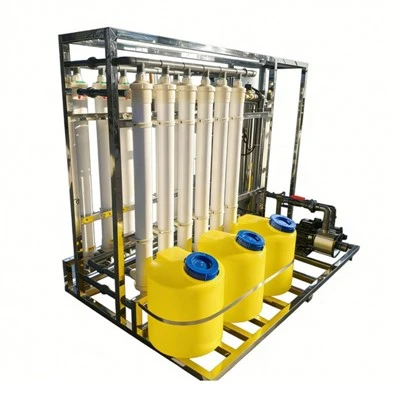
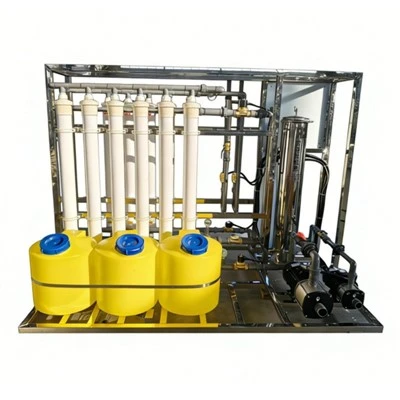
The ROP-IND series industrial reverse osmosis equipment provides high-purity water generation for continuous manufacturing processes. Built on a structural carbon steel or 304 stainless steel skid, each system integrates multi-stage pre-filtration, high-pressure pump assemblies, spiral-wound polyamide composite membranes, and automated PLC control.
Successfully deployed in over 40 industrial facilities across North America and Europe since 2022, the unit reduces total dissolved solids (TDS) by 98.5% to 99.4%, delivering consistent water quality for industrial utilities and production lines. Systems are configured based on raw water chemistry, required recovery rates, and daily volume demands.
-
![Commercial RO Purified Water System]() Commercial RO Purified Water System• 1000L/H high output, 98% salt rejection, stable for commercial water supply.view more
• Smart monitoring & auto-protection, easy operation, low maintenance cost.
• Certified factory, customizable, global one-stop export service. -
![Industrial RO Water Purification System]() Industrial RO Water Purification System· Industrial dual‑membrane purification, 98% salt rejection, stable compliant water output.view more
· Fully automatic intelligent control, water & power saving, low operating cost.
· Flexible customized capacity, adaptable to... -
![Automatic RO Water Purifier]() Automatic RO Water Purifier· Fully automatic operation, zero manual intervention.view more
· Multi-stage filtration, stable pure water output.
· Flexible customization, wide application scenarios. -
![Livestock Farm RO Water Purifier]() Livestock Farm RO Water Purifier· 97% deep purification ensures drinking-grade water, reducing livestock disease rates.view more
· SUS304 stainless steel, rust-proof & stable in harsh farm environments.
· Fits well/tap water, low-maintenance design saves... -
![River Water RO Purification System]() River Water RO Purification System· Direct river water purification with 99% salt rejection for safe drinking & production.view more
· Heavy-duty stainless steel, modular design, stable & low maintenance.
· Certified factory direct supply, custom solutions &...


Skid-Mounted Modular Assembly: Frame, piping, vessels, and electrical panels are pre-assembled and hydro-tested prior to shipment, minimizing on-site installation time.
Energy-Efficient High-Pressure Hydraulics: Utilizes vertical multistage centrifugal pumps paired with variable frequency drives (VFD) to match operating pressure demands and lower power consumption.
Automated Flush and Cleaning Cycle: Integrated clean-in-place (CIP) connection ports and automated flush sequences reduce membrane scaling and organic fouling.
Corrosion-Resistant Process Piping: Low-pressure lines utilize Schedule 80 UPVC; high-pressure concentrate and feed lines utilize 304 or 316L stainless steel with sanitary welds.
Instrumentation & Real-Time Monitoring: Inline sensors continuously measure permeate conductivity, system pressure, pH, and flow rates, feeding data directly to the central PLC/HMI interface.
Technical Specifications
|
Parameter |
Specification Range |
Unit / Standard |
|
Permeate Capacity |
5 - 100 |
m3/hr (22 - 440 GPM) |
|
Salt Rejection Rate |
>= 98.5% - 99.4% |
Nominal (tested at 25°C) |
|
System Recovery Rate |
70% - 82% |
Configurable per feed water analysis |
|
Max Feed TDS Limit |
<= 2000 |
mg/L (PPM) |
|
Operating Pressure |
1.2 - 2.1 |
MPa (170 - 300 PSI) |
|
Membrane Element Type |
4-inch / 8-inch Spiral-Wound |
Polyamide Composite (FilmTec / Toray equivalent) |
|
High-Pressure Pump |
Vertical Multistage Centrifugal |
SS304/SS316 wetted parts, IE3 efficiency motor |
|
Pre-Filtration |
5-micron Multi-Round Cartridge |
Polypropylene (PP) melt-blown |
|
Control System |
Siemens S7-1200 PLC + 7-inch HMI |
Modbus TCP / Ethernet IP communication |
|
Power Supply |
380V/415V/480V, 50/60Hz, 3-phase |
Custom voltage available upon request |
Boiler Feed Water: Supplying low-TDS makeup water to high-pressure steam boilers to prevent scale formation and turbine blade corrosion.
Food & Beverage Processing: Ingredient water preparation, container rinsing, and clean-up water generation meeting sanitary guidelines.
Pharmaceutical Pre-Treatment: Feeding purified water (PW) distillation stills and multi-effect water generation systems.
Electronics Manufacturing: Providing primary demineralized water for component rinsing and printed circuit board fabrication.
Chemical & Automotive Surface Treatment: Rinsing baths and bath makeup for electroplating, painting, and metal finishing lines.

Customization Options
We engineer systems to match specific plant utility constraints and water chemistry profiles. Customization parameters include:

Metallurgy Upgrades
Upgrading wetted piping and pressure vessels from 304 stainless steel to 316L or Super Duplex stainless steel for high-chloride or corrosive environments.
Antiscalant & Chemical Dosing Skids
Integrated metering pumps and chemical tanks for pH adjustment, sodium bisulfite (dechlorination), or antiscalant injection.


Dual-Pass RO Configuration
Addition of a second-pass RO stage for applications requiring permeate conductivity below 1.0 uS/cm.
Enclosure Options
Weatherproof outdoor FRP/steel enclosures or containerized ISO modular units (20ft / 40ft) equipped with internal climate control and lighting.

Quality Assurance & Manufacturing Standards
Material Traceability
All pressure vessels, piping manifolds, and valves are supplied with mill test reports (MTR) verifying chemical composition.
Factory Acceptance Testing (FAT)
Each completed skid undergoes a 4-hour dry and wet functional test, verifying pump alignment, instrument calibration, and PLC logic response prior to crating.
Weld Inspection
Stainless steel process piping welds undergo argon back-purge welding, visual inspection, and periodic hydrostatic pressure testing at 1.5x maximum operating pressure.
Compliance Certifications
Electrical control panels are fabricated in accordance with UL 508A / CE standards. Components comply with ASME, NSF/ANSI 61, and ISO 9001 quality management protocols.

Remote Diagnostics: PLC panels equipped with secure ethernet ports allow remote troubleshooting and program updates by our engineering team.
Spare Parts Availability: Critical wear items—including O-rings, replacement membrane elements, cartridge filters, and pressure transmitters—are stocked for dispatch within 48 hours.
Documentation Package: Every unit ships with an English technical manual containing P&ID drawings, electrical schematics, instrument calibration certificates, and component maintenance data sheets.
[Download Sample P&ID & Datasheet Package PDF]
On-Site Commissioning Support: Virtual installation guidance is standard; experienced field service engineers are available for on-site commissioning and operator training upon request.
FAQ

Request a Quote
Ready to configure an industrial RO system for your plant? Submit your water analysis report and flow requirements to our engineering team.
Email: engineering@yourcompany-b2b.com
Direct RFQ Submission: [Link to Interactive RFQ Form / System Sizing Calculator]
Typical Response Time: Within 24 business hours with preliminary P&ID and technical proposal.
We're well-known as one of the leading ro purified water equipment manufacturers and suppliers in China, featured by quality products and good price. Please rest assured to buy bulk ro purified water equipment made in China here from our factory. Customized orders are welcome.
automatic reverse osmosis system, Livestock Farm RO Water Purifier, automatic water purification machine